Heavy Duty Pallet Racking Manufacturer: Aceally's CE and AS4084 Certified Storage Systems for Global Warehouses
Sep 20, 2026
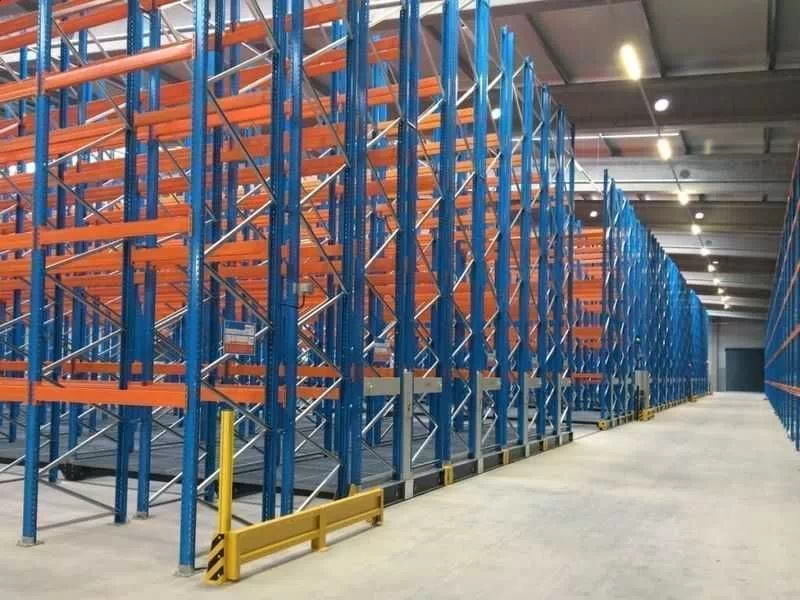
Xiamen, Fujian Sep 20, 2026 (Issuewire.com) - Warehouse logistics managers, industrial facility expansion contractors, and global rack importers face complex engineering decisions when specifying heavy-duty pallet storage infrastructure for high-density distribution centers. As global supply chains expand, logistics facilities require high-capacity storage racks that withstand heavy pallet loads, maintain structural stability under project-specific loading and seismic design requirements, and satisfy strict international safety standards. Partnering with a specialized factory-direct manufacturer such as Aceally (Xiamen) Technology Co., Ltd. (Aceally Group), offering CE-compliant and AS 4084-compliant heavy-duty pallet racking, allows warehouse procurement teams to secure high-grade structural steel systems tailored to regional building codes while avoiding unnecessary intermediary costs. Evaluating heavy-duty pallet racking suppliers requires a structured selection framework to ensure long-term structural integrity, operational safety, and maximum return on warehouse investment.
Drawing from 30 years of practical manufacturing experience in industrial storage systems, Aceally Group highlights four core evaluation dimensions for global warehouse procurement managers specifying heavy-duty pallet racking:
Structural Steel Grade and Load Engineering: Utilizing prime Q235B structural steel, cold-formed profiles, and rigorous load-bearing calculation standards.
Global Regulatory Certification and Compliance: Adhering to Australian AS4084, European CE, ISO 9001 quality management, and international engineering guidelines.
Seven-Step Surface Protection Workflow: Implementing a 7-step quality-controlled process covering pretreatment, multi-layer coating, ISO salt-spray testing, and protective delivery.
Factory Execution and Manufacturing Scale: Operating 150,000 square meters of manufacturing space across four production facilities equipped with automated roll-forming lines and robotic welding.
Q235B Structural Steel Engineering and Load-Bearing Capacity
The structural integrity of a heavy-duty pallet rack depends fundamentally on raw material quality and profile engineering. Low-grade steel profiles subject to heavy pallet loading risk structural deflection, beam sagging, or catastrophic rack collapse. Aceally Group constructs heavy-duty pallet racking systems using high-grade Q235B structural steel, providing optimal tensile strength, yield performance, and mechanical toughness. Cold-formed upright columns and box beams undergo precision roll-forming to create rigid structural profiles capable of supporting heavy industrial pallet loads across multi-tier storage configurations.
Engineering teams analyze beam deflection limits, upright column buckling factors, and load distribution mechanics across every racking layout. Each beam-to-column connection utilizes heavy-duty connector hooks and safety locking pins that prevent accidental beam dislodgement during high-speed forklift loading. Heavy-duty baseplates anchor upright frames securely to concrete warehouse floors using expansion bolts, ensuring structural stability under dynamic forklift impacts and project-specific loading conditions. This rigorous steel selection and mechanical engineering framework ensures that storage systems maintain physical stability across heavy industrial applications.
Regulatory Certification: CE, AS4084, and International Engineering Standards
Regulatory compliance is a fundamental benchmark that ensures operational safety and structural reliability when procuring warehouse racking systems for international projects. Aceally Group manufactures storage solutions under an ISO 9001-certified quality management framework, supporting CE compliance and AS 4084 compliance, as well as applicable design and engineering requirements. These credentials and technical documents support the verification of structural engineering, material specifications, and manufacturing tolerances against relevant project and market requirements.
To support smooth international facility commissioning, Aceally's structural calculations incorporate established regional design codes, including American RMI guidelines, European FEM codes, and OSHA safety standards, where applicable to specific projects and market requirements. This comprehensive compliance foundation provides logistics contractors, warehouse owners, and regional distributors with technical and project documentation to support facility approval, installation, insurance review, and long-term asset management across global markets.
Selective Racking vs High-Density Systems: Access Strategy and Layout Selection
Selecting the optimal heavy-duty racking configuration requires evaluating warehouse storage density against pallet accessibility requirements. Engineered by Aceally Group for high-throughput distribution hubs, the industrial selective racking system for warehouses represents the most versatile storage format, offering 100% direct pallet access for fast-moving inventory. Featuring adjustable horizontal box beams and rigid vertical frames, selective racking accommodates diverse pallet sizes, simplifies stock rotation, and can operate with conventional forklift equipment depending on aisle configuration and warehouse layout.
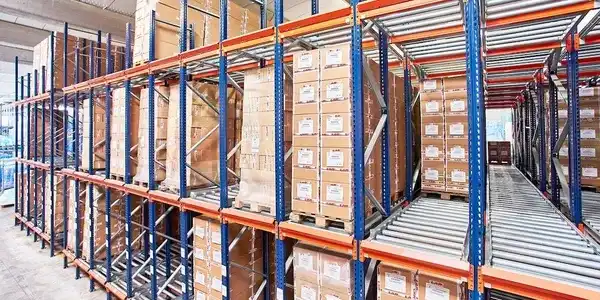
For facilities prioritizing maximum spatial density over 100% immediate accessibility, alternative storage formats engineered within Aceally Group's product range provide specialized operational advantages. Double deep pallet racking arranges selective frames two rows deep, expanding storage capacity while operating with deep-reach forklifts. Drive-in racking eliminates inner operator aisles by allowing forklifts to enter storage bays directly, achieving high space utilization for low-SKU bulk inventory. To satisfy complex storage requirements, pushback, Very Narrow Aisle (VNA), and automated Radio Shuttle systems offer further density options, allowing warehouse managers to deploy layout configurations that optimize total operational throughput.
Seven-Step Surface Preparation and Quality-Controlled Finishing
Surface finishing determines the structural lifespan and long-term maintenance overhead of heavy-duty warehouse racking. Storage systems deployed across diverse global climates--from high-humidity coastal logistics parks to unconditioned industrial centers--require advanced surface engineering to prevent oxidation, coating flaking, and structural corrosion. To ensure consistent durability across international export markets, Aceally Group applies a standardized 7-step surface protection and delivery workflow under technical standard TS-PRC-2026-01.
The process begins with strict raw material inspection to eliminate steel burrs and surface oils before chemical pretreatment. Steel profiles undergo alkaline degreasing (5%-10% solution at 40-60°C for 8-15 minutes) to clear rolling lubricants, verified by ISO 8502-1 and ISO 8502-2 water-break inspection tests. After a two-stage neutral water rinse under ISO 8502-9, components receive crystalline zinc phosphating under ISO 9717, creating a 3-to-8-micron base layer that significantly optimizes paint bonding and corrosion resistance.
The racking components then receive multi-layer protective finishes--utilizing electrostatic thermosetting resin powder coatings for interior warehouses or heavy-duty hot-dip galvanizing for harsh outdoor and saline environments. Following high-temperature thermal curing (70-90°C) to achieve high surface hardness, every production batch undergoes rigorous QC testing, including ISO 2409 cross-cut adhesion tests and ISO 9227 salt spray evaluations (200+ hours with zero blistering). Finally, finished products are secured with ISO 780 compliant protective packaging and installation documentation, guaranteeing that factory-grade structural protection remains intact from international ocean transport to final site commissioning.
Factory Execution and Manufacturing Scale
Verifying a manufacturer's physical production capacity is essential for securing stable lead times on large-scale warehouse projects. Operating as a factory-direct manufacturer rather than a trading intermediary, Aceally Group manages 150,000 square meters of modern manufacturing space across four production bases, including its primary Nantong manufacturing plant. Supported by a workforce of over 600 skilled employees, the facility operates specialized production machinery designed for high-volume rack fabrication.
Production infrastructure includes automated upright roll-forming lines, precision beam roll-forming machines, robotic welding stations, and high-capacity automatic powder coating lines, supported by more than 50 specialized processing machines. Incoming steel coils undergo strict quality control under ISO 9001, verifying surface cleanliness and thickness tolerances before entering processing. Robotic welding systems produce consistent and reliable weld quality on beam connectors and baseplates, eliminating manual welding flaws. This integrated manufacturing control enables consistent component precision, reliable delivery timelines, and stable volume production for international warehouse projects.
Advantages of Sourcing from a Specialized Heavy Duty Racking Manufacturer
Sourcing heavy-duty pallet racking directly from a specialized manufacturer enables warehouse buyers to benefit from traceable material specifications, applicable CE and AS 4084 compliance documentation, controlled surface protection processes, and factory-backed quality control. Compared with sourcing from suppliers with limited product traceability, direct manufacturer engagement can make it easier to verify steel grades, weld quality, load capacities, engineering documentation, and production standards.This direct factory partnership model provides global warehouse operators with verified load capacities, long-term structural durability, and dependable commercial value, while supporting more efficient project communication, technical coordination, and delivery management.
Conclusion
Specifying heavy-duty pallet racking for global warehouse projects requires evaluating structural steel quality, international safety certifications, surface treatment technology, and factory manufacturing scale. By partnering with an ISO 9001 certified manufacturer offering applicable CE and AS 4084 compliance, warehouse procurement managers can deploy high-performance storage systems tailored to specific operational requirements. Utilizing this structured selection checklist allows logistics operators to build safe, durable, and cost-effective warehouse storage infrastructure that supports long-term commercial growth.
To request custom warehouse racking layout designs, download technical product specifications, or discuss volume order lead times for heavy-duty pallet racking, visit the official solution portal: https://www.acerackingsystem.com/warehouse-racking/. For direct engineering consultations, contact the technical sales team.
Media Contact
Aceally (Xiamen) Technology Co.,Ltd.
+86 15960833356
Unit 1003, No. 625 Sishui Road, Huli District, Xiamen , China
Source :Aceally (Xiamen) Technology Co.,Ltd.
This article was originally published by IssueWire. Read the original article here.
More News




YOUR NEWS, OUR NETWORK.
Do you have Great News you want to tell the world?
Be it updates about your business or your community, you can make sure that it’s heard by submitting your story to our network reaching hundreds of news sites across 6 verticals.